Compare practical options for connector pin position and damage checks, including what each route needs, where it fits and what to check before you decide.
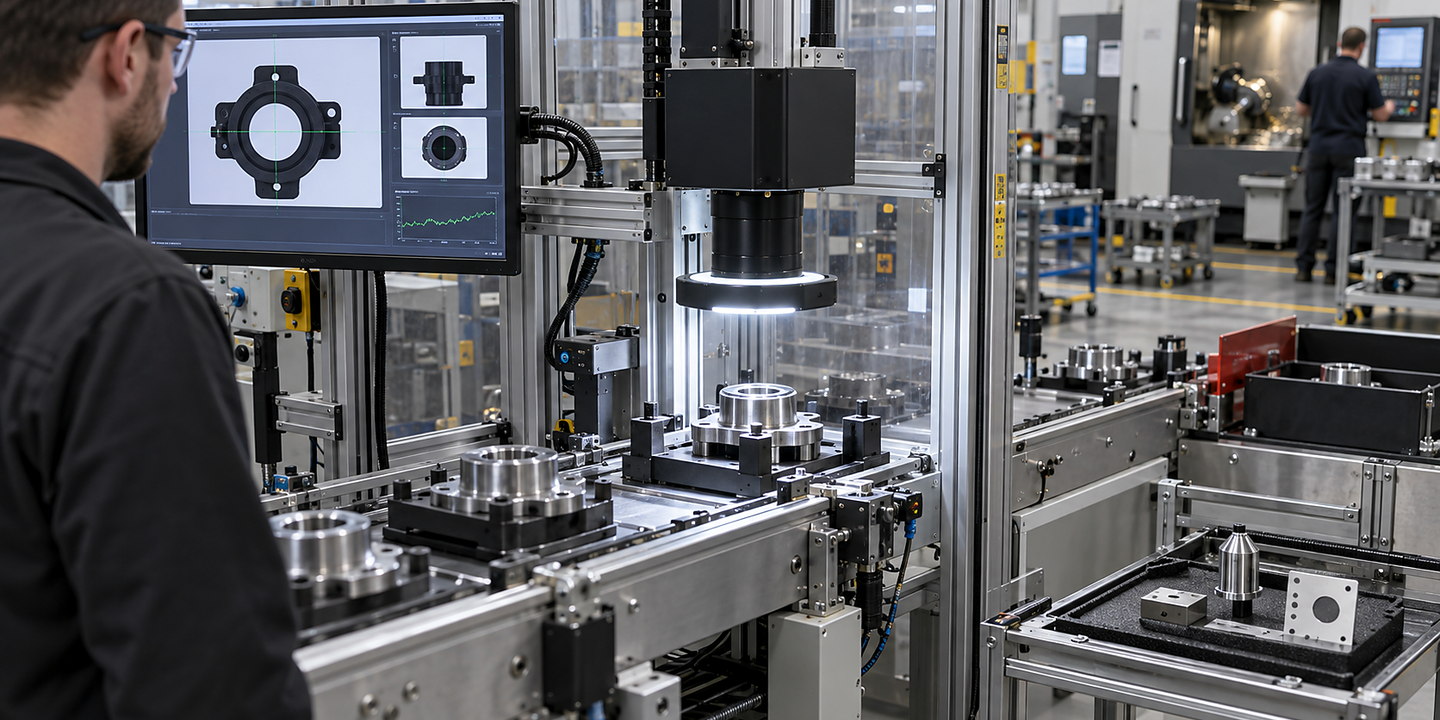
Photographs illustrate general industrial inspection. Connector pin position and damage checks must be proved with representative connectors, defined limits and the intended views.
In brief
The right solution for connector pin inspection is the simplest system that reliably handles your stated duty, line connections and expected exceptions.
Plan connector pin inspection around representative good, bad and marginal samples, line presentation, lighting, reject handling and challenge criteria. Discuss an optical feasibility trial with Oxford Vision Systems.
On the production floor
See how the complete system fits your production line — Connector Pin Inspection
Plan connector pin inspection around representative good, bad and marginal samples, line presentation, lighting, reject handling and challenge criteria. Discuss an optical feasibility trial with Oxford Vision Systems. When you compare solutions, check how each option handles visible defect or measurement definition for connector pin position & damage checks, good, bad and marginal sample range and your surrounding line.
Connector Pin Inspection support from first review to production use
Understand your requirement
Review visible defect or measurement definition for connector pin position & damage checks, good, bad and marginal sample range, and part presentation and production speed using your samples, drawings and production observations.
Compare suitable approaches
Run focused trials for connector pin inspection so you can see why an option is recommended or ruled out.
Fit the complete line
Resolve optics, lighting and environmental conditions, recipe, reject and line-control interfaces, controls, safety, operator access and maintenance before site work.
Prove and support the result
Check false-accept, false-reject and challenge criteria in normal, difficult and fault conditions, then agree training and support for your team.
Typical support: defect definition, sample study, optical trials, enclosure and reject integration, and challenge validation.
Compare your options
Compare connector pin inspection with simpler routes
Approach
Often suitable when
Watch for
Connector Pin Inspection
You need a dedicated solution for a clearly defined duty, product or part range and line interface.
A camera can only assess a property made visible and repeatable by the inspection setup.
Purpose-Built Sensors for Simple Presence or Position Checks
The required decision is a simple presence or position check and trials show that a purpose-built sensor can distinguish the agreed conditions.
Test good, bad and marginal parts at the intended presentation and speed, and define the reject and fault response.
Offline Metrology or Destructive Tests where the Property Is Not Visible Inline
The property cannot be made visible and repeatable in-line, or the required check is hidden, destructive or functional.
Specify the separate test method, representative samples and acceptance criteria; visual inspection does not replace that test.
What to send us
Help us give you useful guidance
Representative Good, Bad and Marginal SamplesInclude the current revision and explain what this information should show for your operation.
False-Accept and False-Reject Challenge ResultsInclude the current revision and explain what this information should show for your operation.
Lighting, Recipe and Reject-Response RecordsInclude the current revision and explain what this information should show for your operation.