Connector Pin Inspection Selection Guide
Compare connector pin inspection using drawings, position limits, visible features, marginal samples and repeatable presentation. Check recipes and line response.
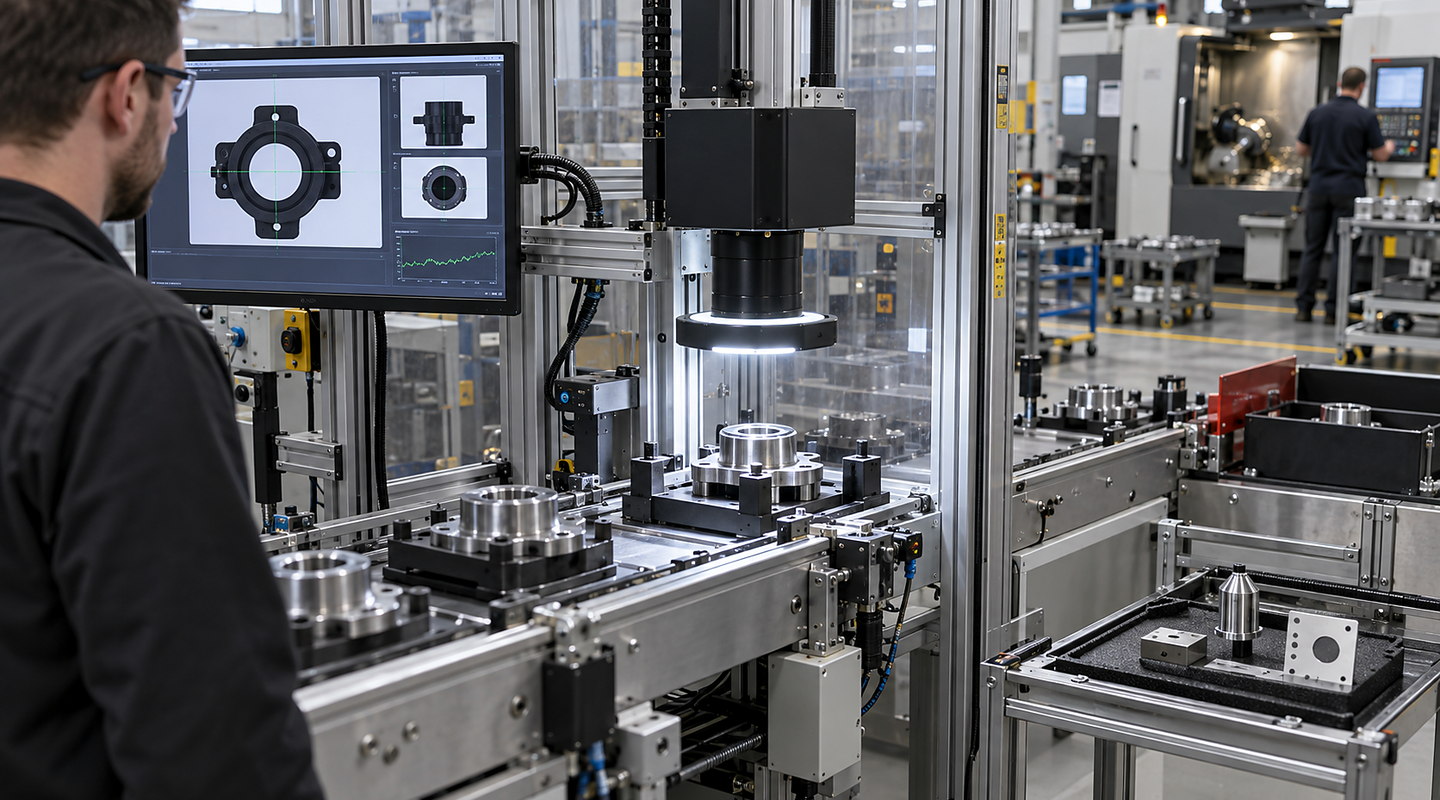
Photographs illustrate general industrial inspection. Connector pin position and damage checks must be proved with representative connectors, defined limits and the intended views.
Compare connector pin inspection proposals against the same drawing, pin layout, allowable limits and identified samples. Require trial evidence that the intended views expose the missing, bent, displaced or partially inserted features under actual presentation and timing. Keep hidden or functional properties outside the claimed visual check.
Use the connector specification checklist and the same acceptance challenge record for every option. A sensor may suit a simple visible presence or position decision if representative trials support it.
Compare options in the conditions where they must work — Connector Pin Inspection
Plan connector pin inspection around representative good, bad and marginal samples, line presentation, lighting, reject handling and challenge criteria. Discuss an optical feasibility trial with Oxford Vision Systems. A useful shortlist should show how every option copes with visible defect or measurement definition for connector pin position & damage checks and recipe, reject and line-control interfaces.
Discuss your application
Ask every supplier the same questions
| Decision | What to ask | What to check |
|---|---|---|
| Visible Defect or Measurement Definition for Connector Pin Position & Damage Checks | Which missing, bent, displaced or partially inserted features must be distinguished, and what position limits define acceptance? | Connector drawings, pin arrangement, allowable limits, required views and explicit features excluded from the visual check. |
| Good, Bad and Marginal Sample Range | Do the samples include good connectors, known defects and marginal cases near every relevant boundary? | Identified representative samples with expected results, connector variants and relevant batch or upstream conditions. |
| Part Presentation and Production Speed | How is the connector located and presented repeatably at intended production timing? | Trial evidence for actual location and views, variant changes, short stops and recovery, with timing limitations recorded. |
| Optics, Lighting and Environmental Conditions | Does the proposed view and lighting make each required feature visible with adequate contrast? | Representative optical observations, including reflective, dirty or damaged cases where relevant, and a separate method for hidden properties. |
| Recipe, Reject and Line-Control Interfaces | How do recipes, result identifiers and line handshakes connect the connector decision to the required response? | Approved recipe, record association, reject and fault states and controlled restart responsibilities. |
| False-Accept, False-Reject and Challenge Criteria | Which repetitions and challenge results establish acceptance, and what happens after a failed check? | Expected and observed results for good/bad/marginal samples, false accepts, false rejects, agreed actions and remaining limitations. |
Include simpler approaches to connector pin position and damage checks in your shortlist
| Approach | Often suitable when | Watch for |
|---|---|---|
| Connector Pin Inspection | You need a dedicated solution for a clearly defined duty, product or part range and line interface. | A camera can only assess a property made visible and repeatable by the inspection setup. |
| Purpose-Built Sensors for Simple Presence or Position Checks | The required decision is a simple presence or position check and trials show that a purpose-built sensor can distinguish the agreed conditions. | Test good, bad and marginal parts at the intended presentation and speed, and define the reject and fault response. |
| Offline Metrology or Destructive Tests where the Property Is Not Visible Inline | The property cannot be made visible and repeatable in-line, or the required check is hidden, destructive or functional. | Specify the separate test method, representative samples and acceptance criteria; visual inspection does not replace that test. |
Pause before choosing when…
- Only perfect or hand-selected examples of in-line inspection using connector pin position and damage checks are available.
- No one has defined how false-accept, false-reject and challenge criteria will be evaluated.
- The normal range for visible defect or measurement definition for connector pin position & damage checks is described only as “usually fine” but has not been bounded.
- Your operator, cleaning, maintenance or recovery access has not been considered.
- Quoted performance depends on another machine or data source that is not included.